
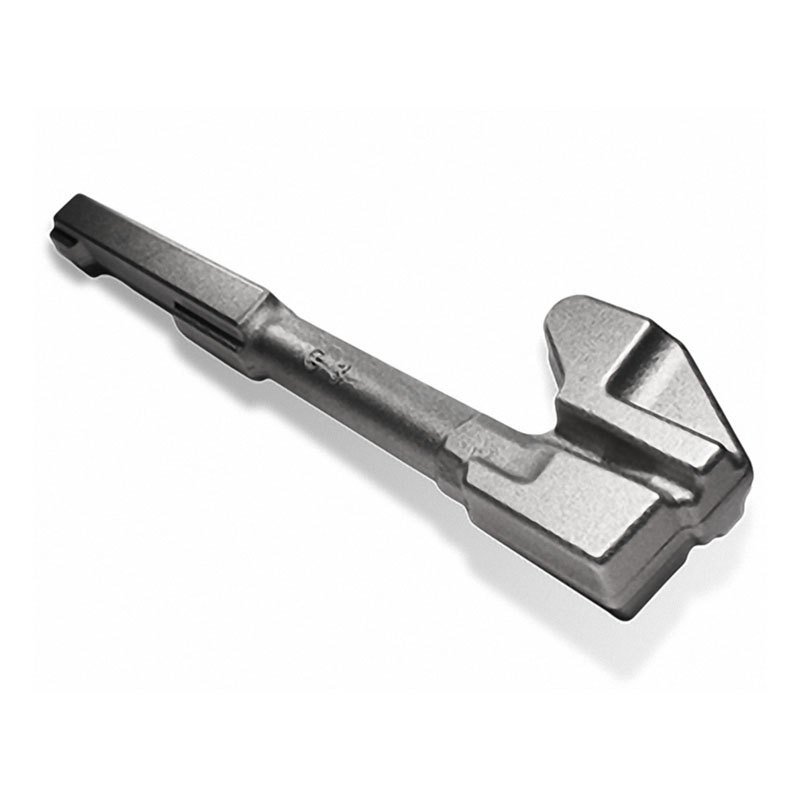
01
Controlled Billet Heating
Heating temperature and time are controlled to obtain uniform plasticity without overheating or excessive scale.
Closed die forging for parts that carry load and cannot afford internal defects.
The billet is heated to the correct forging range and formed in matched dies. Metal flows into the cavity instead of being cut from stock, so the finished part retains a continuous grain structure aligned with its working loads.
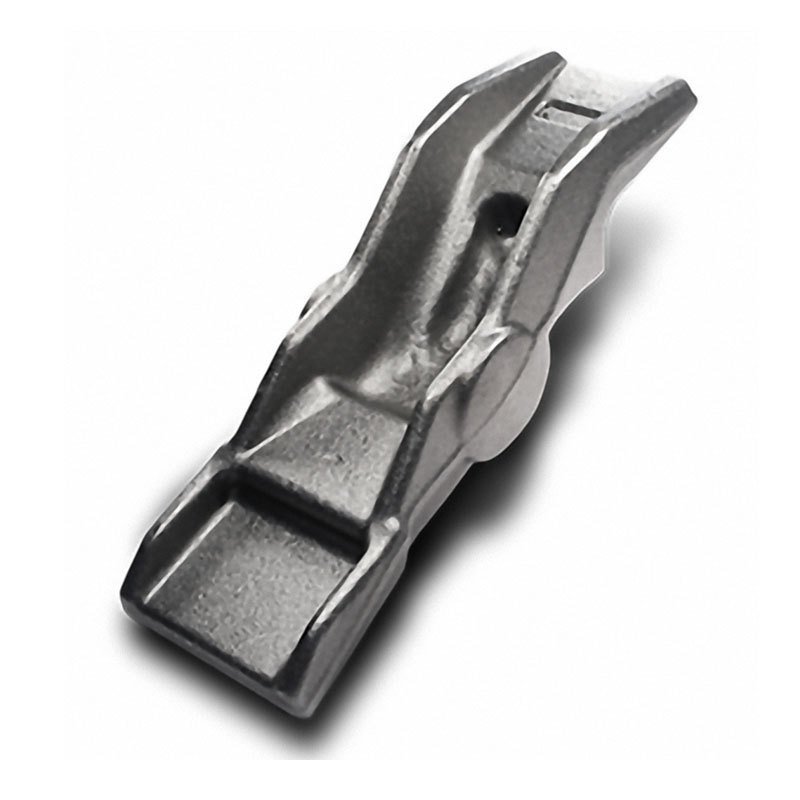
Heating temperature and time are controlled to obtain uniform plasticity without overheating or excessive scale.
Matched dies form the part close to its finished profile, reducing machining allowance and keeping material flow continuous.
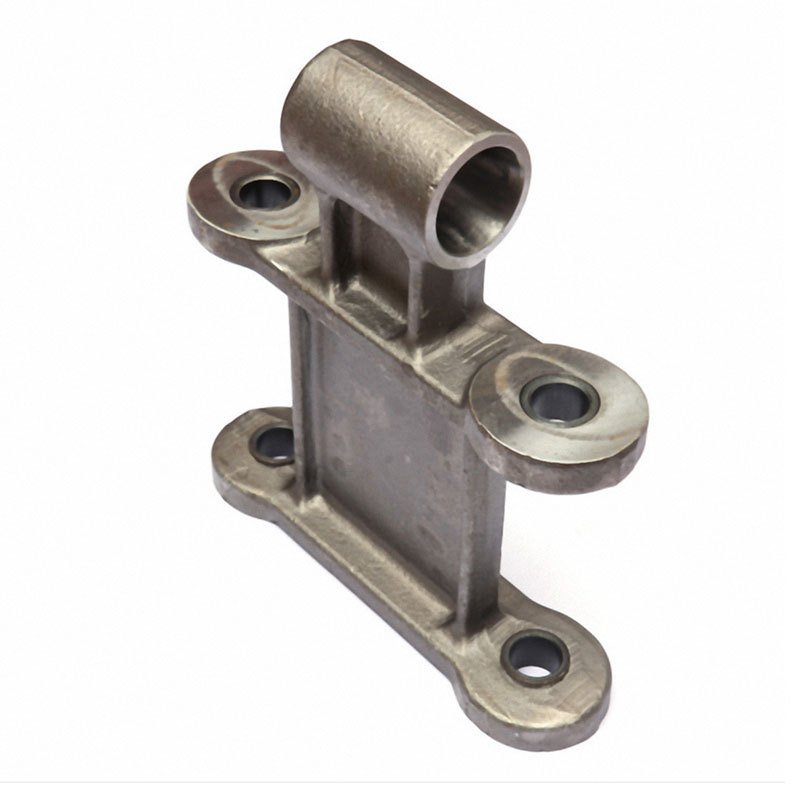
Normalizing, quenching and tempering are followed by CNC turning, milling, drilling and inspection to the drawing.
Carbon steel, alloy steel, stainless steel and selected aluminium grades.
Flanges, gear blanks, yokes, links, levers, bearing rings and safety-critical parts.
Material certificate, hardness, dimensions, MPI or DPI and first article reports.
SPECIALIZING IN FORGING, CASTING AND PRECISION MACHINING FOR CUSTOM METAL COMPONENTS
Request a quoteAttach a drawing or describe the part. Our engineers will reply with process advice, tooling requirement, unit price and lead time.

